 English
 Arabic
 Chinese (Simplified)
 Dutch
 French
 German
 Italian
 Portuguese
 Russian
 Spanish
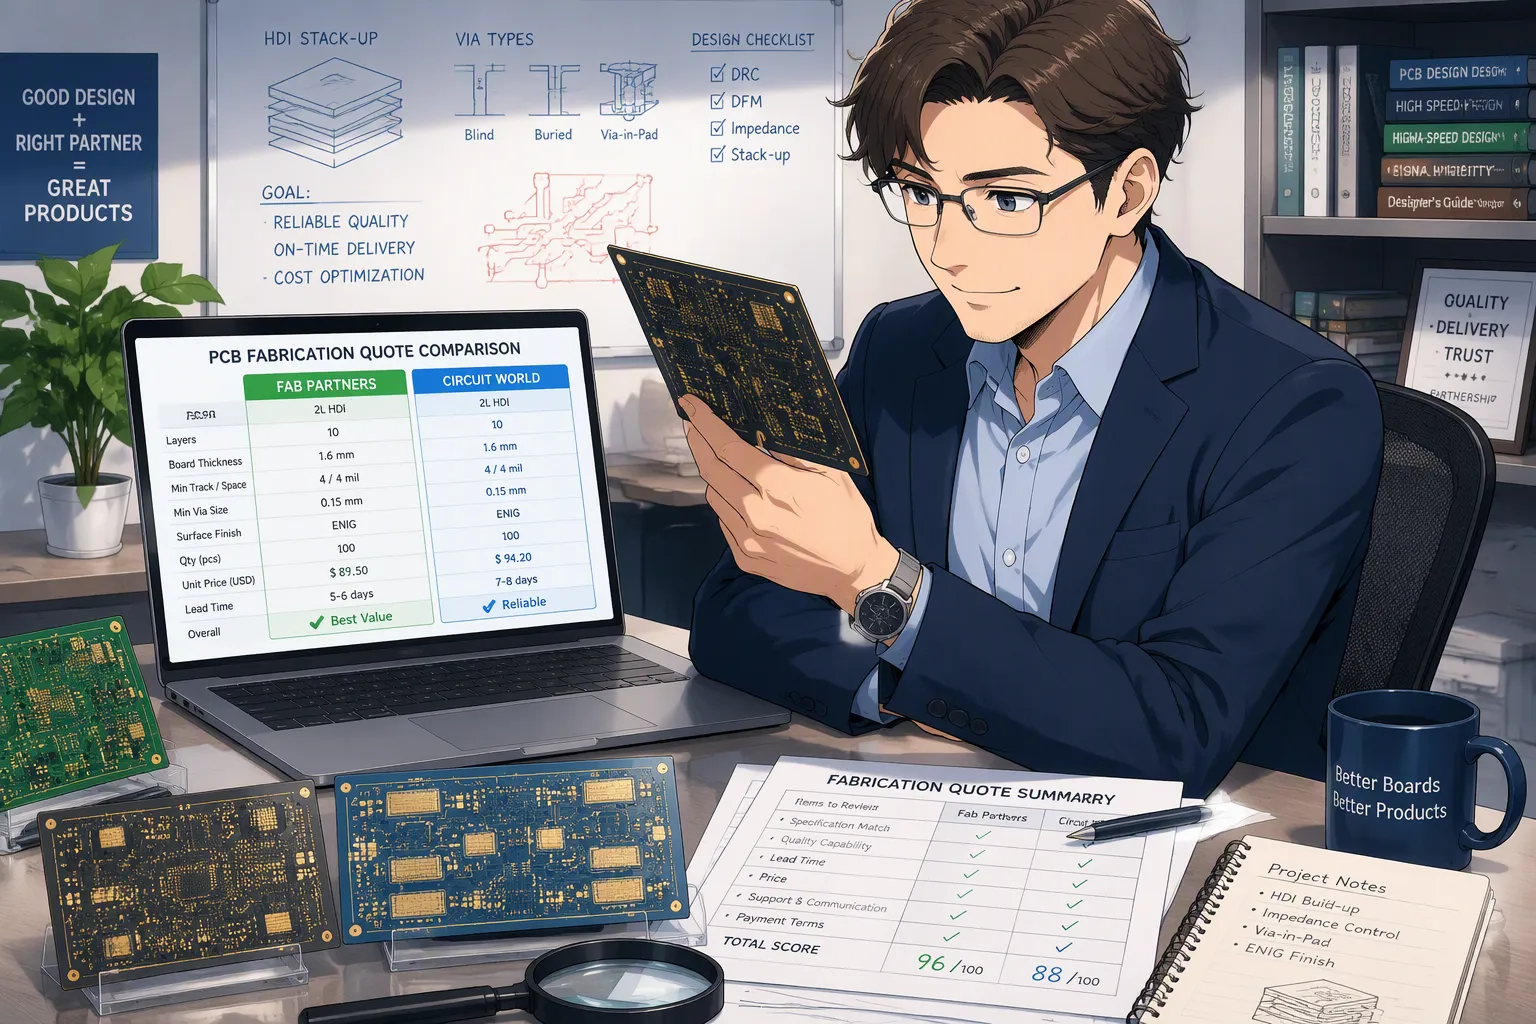
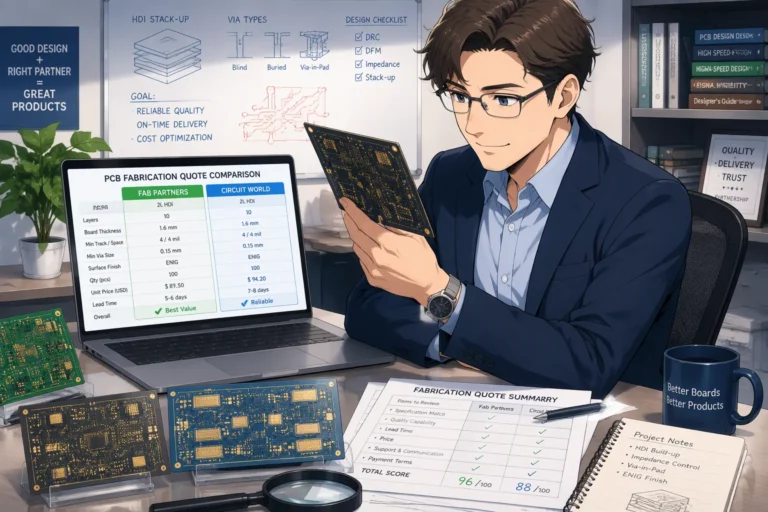
Comparing quotes well means checking every one against the same technical, quality, application, and cost rules. Price by itself hides the real differences.
Buyers often have several quotes with numbers that look alike or oddly low. Those papers do not show which supplier can truly build the board well. A low number may come from a different stackup, thinner copper, or tests the supplier left out.
This article gives a step-by-step plan for hdi pcb fabrication sourcing. It goes from technical details to a list of questions for the supplier. Each quote is then judged on equal footing. The lowest number no longer decides the award by default.
Key Takeaways
Set one standard spec for all suppliers so you can compare them fairly.
Compare technical details like microvia size and line width, not just price.
Look at quality certifications and test reports to make sure the product is reliable.
Pick the PCB stackup that fits what your application needs and its reliability class.
Use a scoring list with different weights to rate quotes and steer clear of hidden costs.
Set a Baseline for HDI PCB Fabrication Quotes
Why Low Quotes Mislead
High-density interconnect printed circuit boards use thin lines, tight spaces, and dense wiring. Two suppliers can price the same design file and still quote different constructions. One treats the job as routine work. The other sees near-limit features and prices accordingly. The numbers are not comparable.
A cheap quote often hides a weaker scope. The table below shows what a low headline price can conceal.
Pitfall when comparing by price only | What the cheap quote may hide |
|---|---|
Material grade and brand | Lower-grade substrates that fail automotive or industrial reliability |
Process and tolerance | Looser impedance control, larger minimum line and space, cheaper surface finish |
Testing scope | Skipped flying-probe electrical test, impedance test, or AOI inspection |
Quality standard | IPC Class 1 instead of IPC Class 3 |
Engineering and DFM service | DFM review and CAM support charged extra or excluded |
A $42 quote against a $38 quote looks simple until one includes X-ray inspection and the other does not. The cheaper number can become the more expensive option once scope is equalized. Buyers should also request a four-bucket cost breakdown up front. A lump-sum quote leaves no way to audit future price changes.
Normalizing Quotes to One Spec
HDI fabrication still uses the same fabrication data as conventional PCBs. That fact makes a single-spec baseline feasible. The buyer freezes one released stackup revision and sends it to every supplier. The package includes identical buildup, copper weight, microvia structure, surface finish, inspection requirements, and quantity. Impedance targets and tolerances stay fixed across all quotations.
The RFQ package should also carry one set of acceptance criteria. IPC-A-6012 serves as the baseline for evaluating HDI rigid PCB quality, with focus on dimensional stability, material quality, and process consistency. Suppliers then price the same released construction, not their preferred version. Any quote built on a different stackup goes back for re-quoting before comparison begins.
Compare Technical Parameters in HDI PCB Fabrication
Microvia, Line Width, and Layer Count
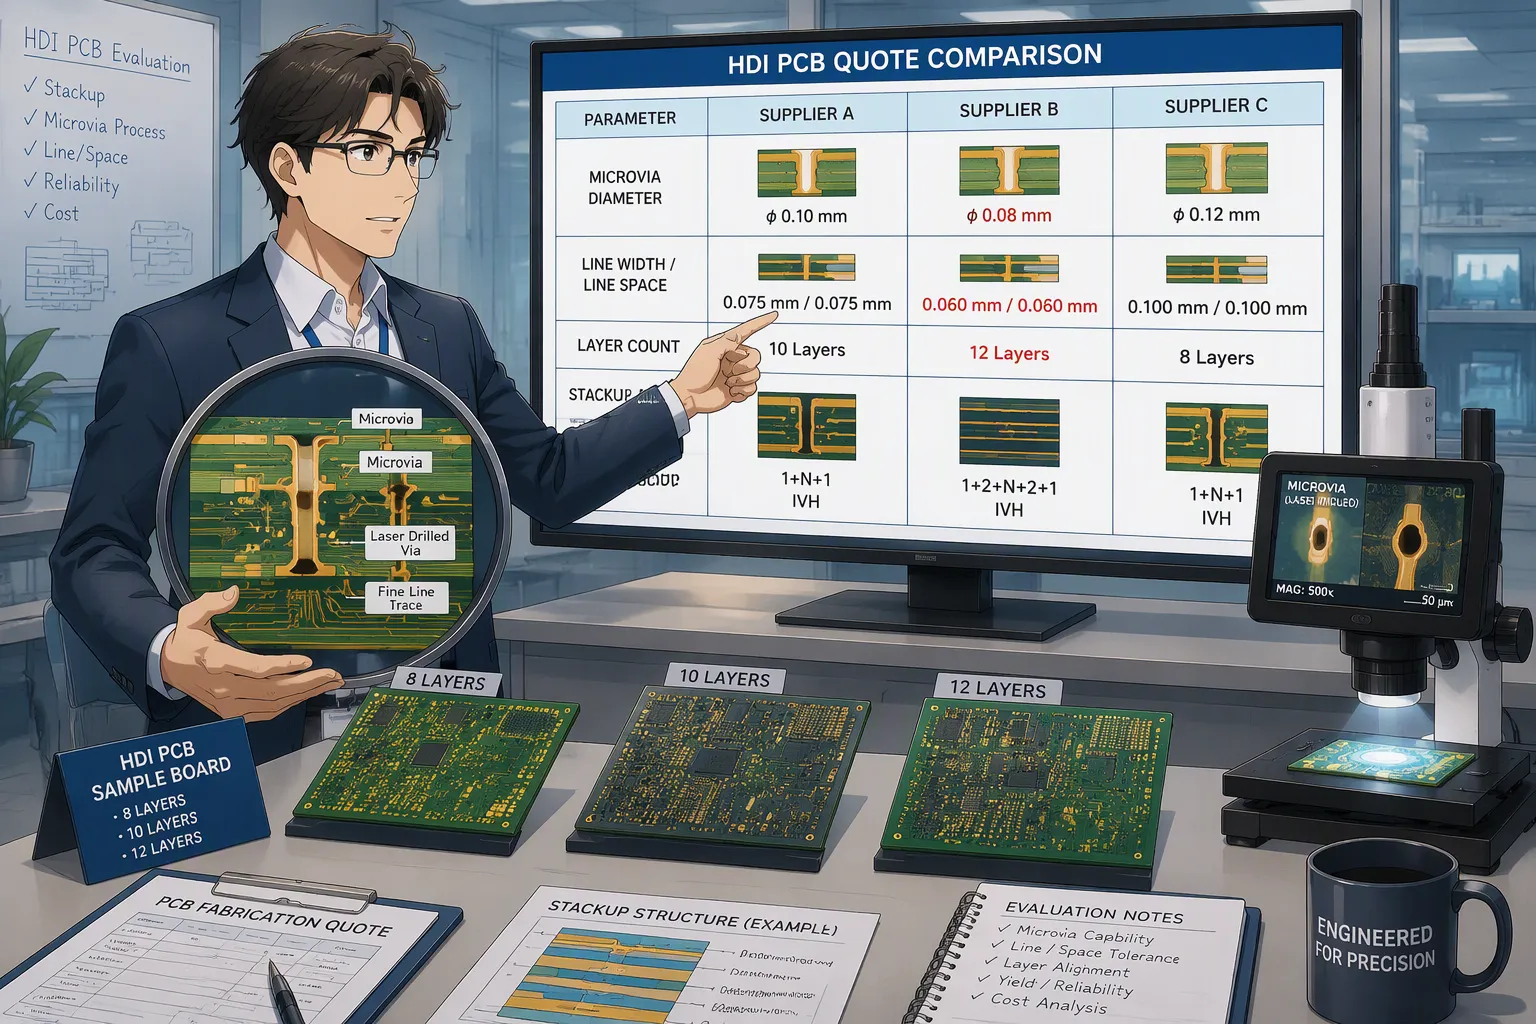
A side-by-side table turns scattered quotes into a clear picture. Buyers should list microvia diameter and drill pairs, line width and spacing, layer count, stackup buildup, base materials, surface finish, and dimensional tolerances. Stackup design sets performance, manufacturability, and cost. Quotes built on different stackups must go back for re-quoting to a common stackup before any comparison holds.
Microvia structures drive cost in predictable ways. More sequential laminations add handling, alignment, and yield risk. Stacked and blind microvia structures cost more than staggered vias because they add process cycles. Laser-drilled microvias use up time and consumables, and each via needs precise energy control. Aspect ratio stays below 1:1 for reliable plating, which limits stack height. An 8-layer HDI board is not always cheaper than a 10-layer conventional board, so buyers should judge cost at the system level.
Factor | Effect on Cost and Manufacturability |
|---|---|
Sequential lamination count | More cycles raise cost; three sequential laminations sit at the top |
Stacked vs. staggered vias | Stacked structures add process cycles; staggered vias improve yields |
Laser drilling | Uses up time and consumables; each microvia needs precise energy control |
Via filling | Adds plating, resin plugging, and planarization steps |
Any-layer HDI | Demands the most cycles and multiplies cost |
Line width tells a similar story. HDI design and fabrication supports fine line and space geometries at 2 mil and below. Reliable production at or below 2 mil requires laser direct imaging, controlled etching, and high-precision drilling. The minimum line and space a supplier can hold reliably belongs in every quote comparison. Ultra-HDI designs may need SAP, mSAP, or embedded trace processes, and each quote should state whether the supplier supports them. This is where hdi process capability separates suppliers.
Materials, Surface Finish, and Tolerances
Base material selection shapes signal integrity and reliability. Most HDI dielectrics have a Dk between 3 and 4, and high-frequency designs favor a lower Dk near 3 to 3.5. Lower Dk lets signals travel faster and reduces crosstalk between tightly packed traces. Dissipation factor matters too, since low-Df materials cut attenuation and localized heating. Buyers should confirm the quoted laminate grade, Tg, and CTE against the application.
Surface finish affects both assembly yield and cost. ENIG offers a flat, planar surface for fine-pitch parts and costs roughly $0.30–$0.60 per square inch. HASL costs less but suits through-hole or larger SMT parts better. Immersion silver sits between them on price and performance. Tight impedance control and controlled impedance verification belong in the quote scope, not as afterthoughts. Dimensional tolerances, including layer-to-layer registration, should appear as explicit values.
When selecting a surface finish, weigh cost and process complexity against performance, since superior finishes may require more intricate processes and higher costs.
This hdi process and technology capability review exposes weak quotes early. A supplier that cannot state its microvia process or its controlled impedance limits has not priced the real job.
Check Quality Systems at Top HDI PCB Manufacturers
Certifications and IPC Class
What a certificate covers matters as much as the certificate itself. Buyers should check IPC class, ISO registration, and IATF where automotive work applies. The audit scope must include HDI build-up work, not just rigid PCB fabrication. A supplier with a strong rigid board record may still lack documented HDI process control.
IPC class drives both cost and reliability. Class 2 suits consumer, industrial, and telecom HDI production, where minor non-functional defects are acceptable and faster lead times matter. Class 3 fits medical, aerospace, and automotive safety boards, where constant performance is required. The table below shows how the two classes differ.
Aspect | IPC Class 2 (HDI) | IPC Class 3 (HDI) |
|---|---|---|
Cost | Baseline | 15–40% higher |
Annular ring | 90° breakout often acceptable | No breakout; continuous ring |
Copper plating | ~20 µm average | Minimum 25 µm average |
Inspection | Sampling plus AOI | 100% AOI, X-ray, cross-section |
Inspection standards separate the two classes more than anything else: Class 2 allows minor annular ring breakout and about 20 µm average plating, while Class 3 requires full continuous rings and 25 µm minimum void-free plating.
Test Evidence and Traceability
Quality claims in a quote mean little without documents to back them up. Buyers should ask for material and stackup verification, laser microvia inspection reports, and microvia plating and filling checks. These records confirm microvia integrity and support proven interconnect reliability. Sequential lamination and registration data, AOI and X-ray results, and 100% electrical and impedance test reports complete the package.
Traceability closes the loop. Lot-level records tie each board to its laminate batch, drill program, and test results. Environmental and thermal cycling data, when offered, strengthen validated reliability testing claims. Buyers should treat reliability testing evidence as a must, not a bonus. Suppliers that state quality systems and certifications without paperwork have not shown reliability controls. Documented reliability testing and clear quality certifications give buyers a solid basis for awarding work to hdi pcb manufacturers. Strong quality systems and certifications at hdi pcb manufacturers protect long-term interconnect reliability.
Match HDI Rigid PCBs to Your Application
How Application Drives Stackup Needs
The application’s needs decide the stackup before price matters. Signal density sets the layer count and routing space. Thermal load sets the copper weight and cooling method. Reliability class sets the material grade and how deep the inspection goes. A consumer board and a medical board can share a netlist and still need different builds.
Suppliers of hdi rigid pcbs use advanced processes to meet aerospace, automotive, and medical demands. These processes include complex interconnection, BGA fanout, ELIC, and cooling techniques. HDI designs also follow IPC and other international standards, so boards work reliably in defense systems, medical devices, and industrial automation. The stackup design guide lists the applicable reliability standard as a selection criterion. That link means the end application’s reliability class directly limits the stackup choice, and every quote must show it.
Any-layer HDI shows the trade-off clearly:
Microvias connect any layers for the most routing flexibility and density.
High-end smartphones, medical devices, and aerospace applications use it.
Multiple lamination and laser-drill steps make it very expensive, and yield can drop.
An engineering review at quote time is therefore needed for costing. Buyers should confirm that quoted microvia structures and laser-drilled microvias match the application class, not a generic build.
DFM Support Before You Commit
A DFM review belongs before the quote is final, not after the order. Early DFM work catches critical via sizing, stackup optimization, and design review feedback while changes cost little. Suppliers should offer dfm before layout release so that controlled impedance targets and microvia structures are settled in the data package. This step protects interconnect reliability and keeps the quoted price honest.
Buyers should treat dfm as a scored service, not a courtesy. A supplier who quotes to its own preferred spec rather than the buyer’s requirements should re-quote to those requirements. Strong dfm support and clear reliability evidence separate engineering-grade fabricators from budget shops. The goal is a quote whose assumptions, capabilities, and costs are fully visible.
Compare HDI PCB Manufacturers on Total Cost
Tooling, Testing, and NRE
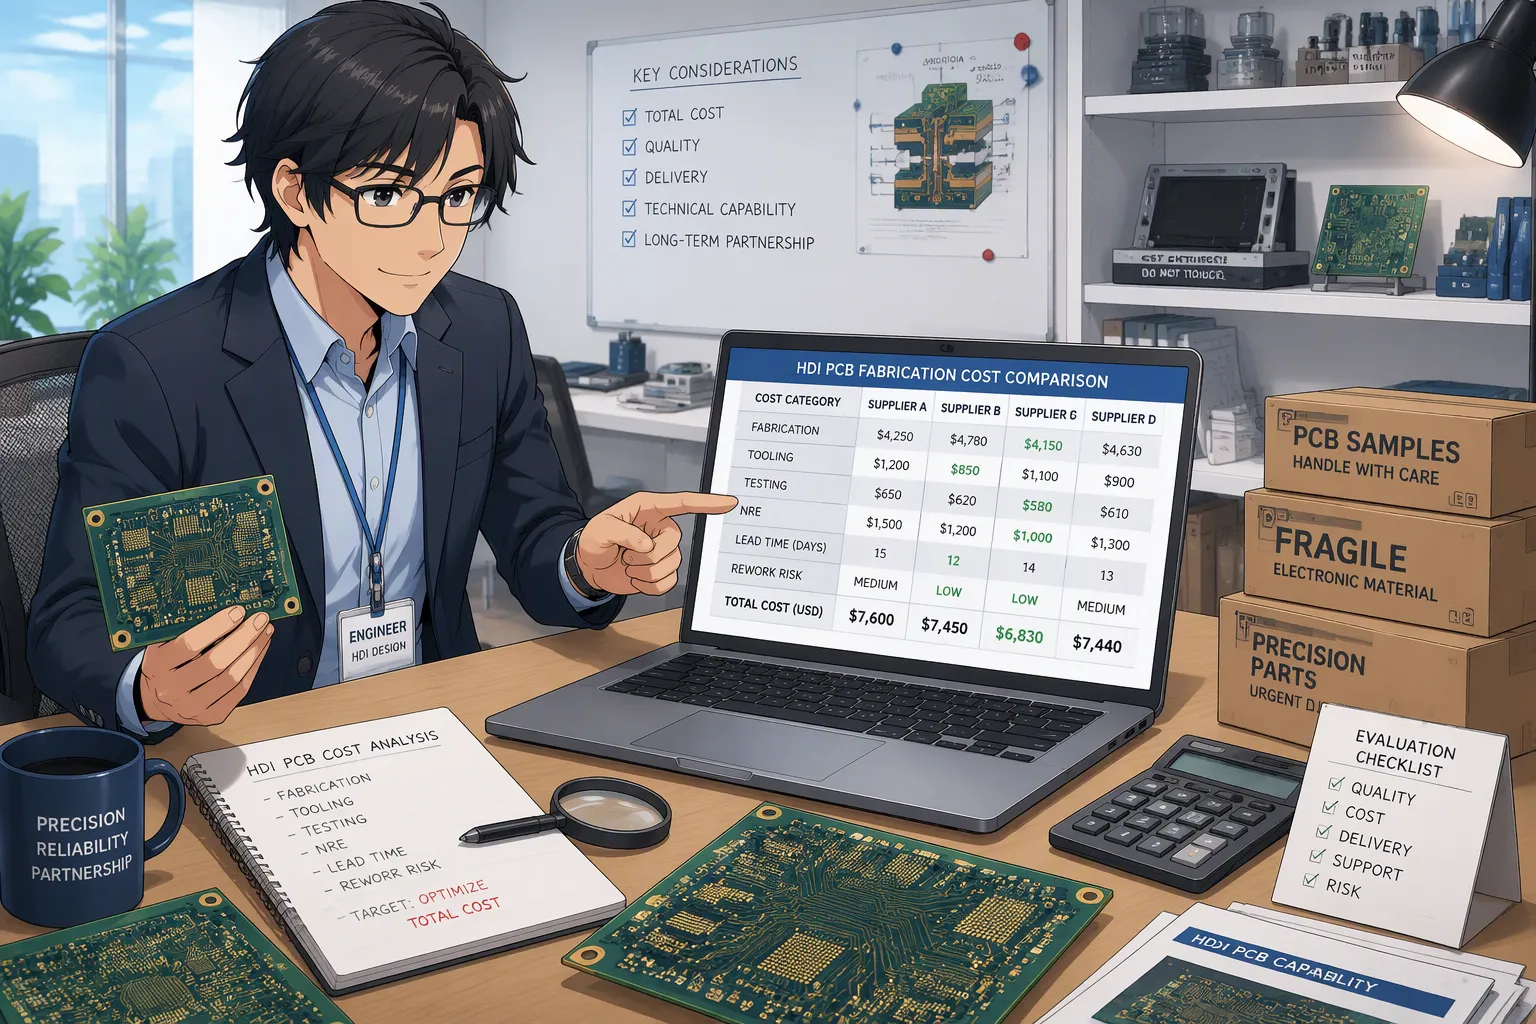
Unit price is just one line on the invoice. Before ranking hdi pcb manufacturers, buyers should list tooling, test fixtures, NRE, panel utilization, and logistics. A low unit price with a big NRE charge can cost more on a small build. Panel utilization changes the real price per board, since a stackup that wastes panel area creates more scrap. Freight and logistics belong in the same ledger.
Lead Time and Rework Risk
Lead time changes the real cost in ways the unit price never shows. The table below links each effect to its cost impact.
Lead-time effect | Cost impact on total fabrication cost |
|---|---|
Delayed product launches | The cost of delay often exceeds the added PCB unit cost |
Increased buffer inventory | Higher carrying and inventory costs |
Less flexibility for late design changes | Rework and redesign costs |
Capacity limits for HDI and automotive PCBs | Locking in capacity early matters more than small price cuts |
Material trends in laminate, copper, fiberglass, and resin | Add cost pressure, especially for high-layer and HDI designs |
Shorter lead times come with their own trade-offs. They can raise component cost, may need overtime production, and cut sourcing flexibility. HDI boards with blind or buried vias need sequential lamination and extra process steps. Microvias and stacked microvias need tighter registration and more lamination cycles. These steps make lead time longer and add processing cost to hdi pcb fabrication.
Rework risk is a big factor at fine pitch. Localized rework heat can affect nearby joints at ultra-HDI pitch, which raises the chance of collateral reflow or damage. Teams then buy special equipment or accept higher scrap rates. Both outcomes raise total cost. The table below shows a monthly rework and scrap estimate.
Cost component | Basis and rate | Resulting cost |
|---|---|---|
Rework labor | 20 min per board at $30/hr ($7.50/board) across 750 boards | $5,625 |
Scrap losses | 10% of defective boards (75 units) beyond repair at $15/board | $1,125 |
Total direct cost | Rework plus scrap for the month | $12,750 |
Torn traces and burned pads can turn a repair into full scrap, and hot air stations and microscopes add expense. A simple scoring matrix should weight capability, evidence, cost, lead time, and DFM support. Budget shops with basic 1+N+1 buildup fit best for lower-density consumer and industrial hdi rigid pcbs with moderate reliability needs. Engineering-grade fabricators fit best for high-layer, any-layer, and safety-critical work. Neither choice is wrong; the application decides.
Score Quotes with a Supplier Checklist
Questions That Expose Assumptions
A checklist helps turn unclear quotes into facts you can check. Buyers should ask which stackup the supplier quoted, which microvia process it used, which tests the price includes, and what the price leaves out. The answers show whether a quote is real or just a rough guess.
What a clear quote must state | Warning signs that point to hidden assumptions |
|---|---|
Tooling and setup fees listed plainly | “Call for final price” |
Shipping costs estimated | No breakdown given |
Rush service pricing | A price that is far too low (under half of the others) |
Engineering support fees | Many vague “fees” |
Remake and warranty terms | No company certifications listed |
Stackup questions need a closer look. Buyers should ask for the exact press stackup used for the quoted build. They can suggest a standard equivalent material in place of the listed laminate and ask the supplier to confirm it works. These checks show whether the supplier quoted the right construction or just its own favorite version.
Via treatment needs the same careful check. Buyers should confirm whether the supplier suggests stacked or staggered microvias and ask for proof of that structure. For via-in-pad, they must confirm the affected lands, layer spans, and the agreed filling and capping treatment. An open via, a filled laser microvia, and a plated-over resin-filled through via are not the same thing.
Weighted Scoring Matrix
A simple matrix turns answers into scores you can compare. Buyers give weight to five areas: capability, evidence, cost, lead time, and dfm support. Each supplier gets a score in each area, and the weights depend on the application. A safety-critical board gives heavy weight to evidence and capability. A consumer board may weight cost and lead time more.
The scores should put suppliers on a shortlist for a follow-up RFQ, not pick a winner. Buyers then re-quote the top candidates to one spec and compare again. This two-step approach helps with sound manufacturer selection across hdi pcb manufacturers and keeps price from deciding alone. It also protects long-term reliability, since documented reliability testing and clear microvia structures carry real weight in the final score. Buyers comparing hdi pcb manufacturers and hdi rigid pcbs should treat the checklist as the last gate before awarding.
A good comparison follows a set order. Buyers set one baseline, compare technical details, check quality evidence, confirm the board fits the application, and add up the real cost. The supplier checklist then works as the last check before awarding.
The goal is not the lowest price. The goal is a quote whose assumptions, abilities, and costs are fully clear and easy to compare.
Buyers should ask for itemized quotes for their next HDI fabrication RFQ. They should use the checklist on every response. That habit turns a pile of similar-looking prices into a clear, defensible decision.
FAQ
How long should an HDI fabrication quote stay valid?
Suppliers should put a validity window in writing. Prices for laminate, copper, and resin change, so a quote with no end date hides risk. Buyers should check that the window covers their decision timeline. They should also ask how the supplier handles material price changes after the order is awarded.
Should buyers request samples before awarding an HDI order?
Samples help when the design pushes process limits, like 2 mil line and space or stacked microvias. For routine builds, documented test coupons and microsection reports may be enough. Buyers should match the amount of evidence to the reliability class of the application.
What if a supplier refuses to re-quote to the buyer’s stackup?
A refusal shows that the supplier prices its own preferred construction, not the released design. Buyers should treat that answer as a capability gap. They should keep the supplier off the shortlist until it quotes to the common spec.
How many suppliers should reach the follow-up RFQ stage?
A shortlist of two or three works well. The weighted matrix narrows the field first, and then the follow-up RFQ compares finalists on one spec. More candidates add paperwork without improving the decision.
Does a basic 1+N+1 buildup quote suit any HDI project?
Yes, for lower-density consumer and industrial boards with moderate reliability needs. Buyers should confirm the application’s signal density and reliability class first. High-layer or any-layer designs need engineering-grade fabricators instead.